Adhesive dispensing · Manufacturing Problems & Solutions
Detect Adhesive Dispensing Defects Early
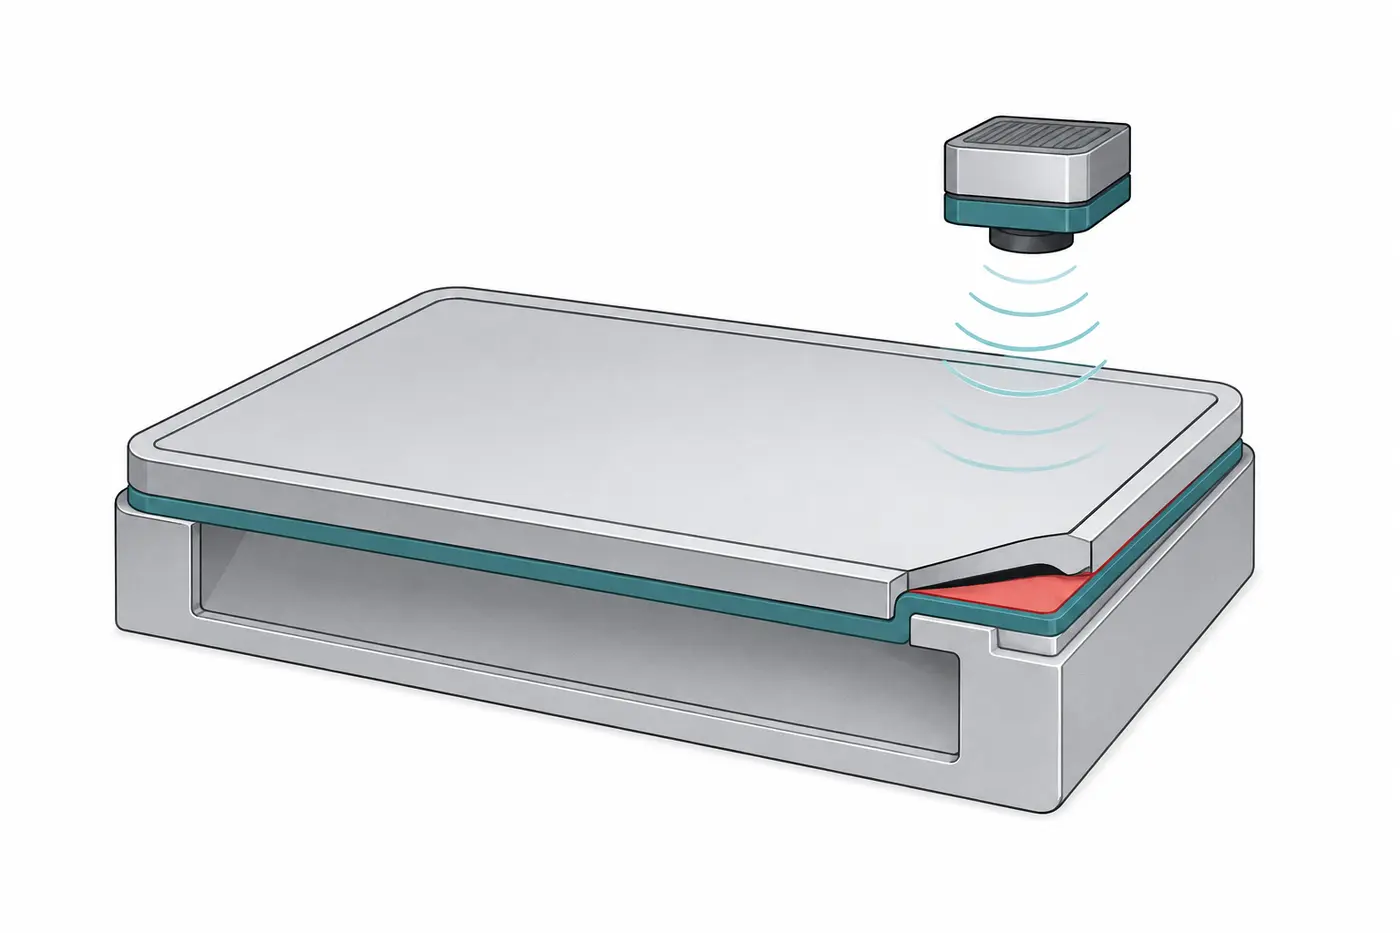
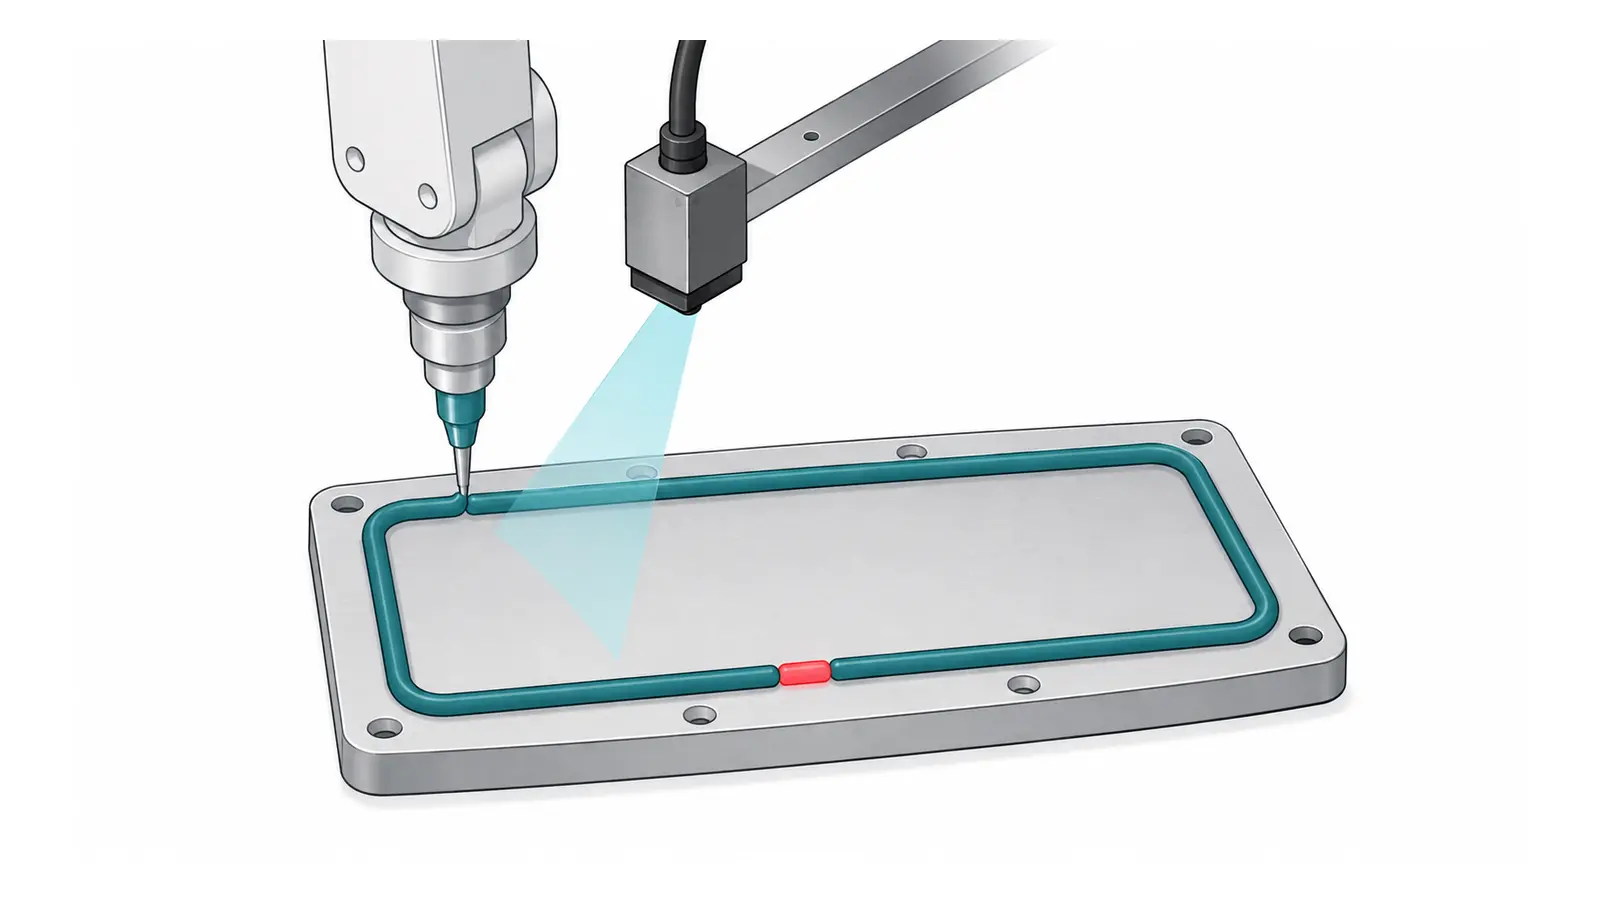
A missing segment, volume error, and poor wetting do not always arise at the same point. We separate bead geometry, mix ratio, and joint effect.
Non-binding · a photo is enough to start · direct contact person
My practical view on adhesive dispensing defects is that an open cause is acceptable; a hidden assumption is not. I would first make the symptom, boundary conditions, and required decision precise enough that two specialists are pricing the same problem.
CorDev uses eXalt® to translate that buyer-side description into testable subquestions. The aim is not to recommend the most impressive technology. It is to find the shortest defensible path from the current manufacturing problem to a decision the team can implement.
Ready in 60 seconds
Three inputs are enough for a credible first assessment
- Observed failureWhat differs from the expected result, and when does it occur?
- Decision requiredFind the cause, evaluate parts, or stabilize a process?
- One referenceIf available: good/failed part, image, drawing, or functional limit.
The real problem
What this request is really about
A request about adhesive dispensing defects should start with the production symptom, not with a preferred vendor or a technology picked too early. The immediate objective is to identify missing material, wrong bead geometry, mixing errors, bubbles, stringing, or process drift before cure. That objective is specific enough to begin supplier discovery while leaving room for a specialist to challenge the first assumption.
In my experience, the useful distinction is between detection, explanation, and prevention. Detection answers whether the condition is present in the submitted part or current production. Explanation connects the condition to material, design, equipment, handling, environment, or measurement. Prevention turns that evidence into a controlled process or inspection decision. Combining all three without saying which outcome matters most produces quotes that look similar but buy different work.
eXalt® from CorDev therefore structures the observed symptom, affected part, operating context, urgency, and expected decision before specialists are approached. The buyer does not need to know the final method. The request remains centered on a real, current manufacturing need and the evidence required to act on it.
Do not lock in too early
Typical drivers and useful first distinctions
For adhesive dispensing defects, the first task is to build an event trail. Useful facts include when the problem began, whether it follows a machine, tool, supplier lot, shift, product variant, environmental condition, or service event, and how good parts differ from bad parts. Identify missing material, wrong bead geometry, mixing errors, bubbles, stringing, or process drift before cure. That statement should be treated as a working investigation goal rather than a predetermined conclusion.
The inspection process also has to be questioned. Fixture changes, temperature, software thresholds, calibration, operator practice, sample preparation, and part presentation can create an apparent quality shift. A repeatability check prevents a team from solving the measurement system while believing it is solving the manufacturing process, or from changing the process to compensate for an unstable measurement.
A good cause map ranks hypotheses by available evidence and business consequence. It does not send every conceivable mechanism to the laboratory. Failed parts should be protected, traceability should be retained, and representative good parts should be collected before corrective actions erase the original conditions. This makes the next test smaller, faster, and more likely to answer the real question.
From assumption to evidence
Which testing or solution paths may fit
Potential evidence paths include 2D and 3D vision, laser profiling, flow and pressure monitoring, weight checks, thermal imaging, and destructive references. These are options, not a shopping list. The right sequence depends on material, geometry, access, defect orientation and size, line speed, allowed sample damage, and the consequence of a missed defect.
I normally prefer a staged plan. The first stage establishes whether the symptom and the good-versus-bad distinction are repeatable. The second stage localizes or characterizes the relevant difference. The third stage confirms cause through a controlled comparison, a targeted trial, or correlation with production data. Only after that should a team decide whether it needs a one-time laboratory result, a sampling plan, or a validated inline solution.
For production deployment, sensitivity alone is not enough. Cycle time, false rejects, false accepts, calibration, reference standards, variant handling, traceability, maintenance, and data interfaces matter just as much. A supplier should explain how the signal becomes a release, containment, or process decision under real operating conditions.
Concrete inspection decision
Four points that determine the method for this failure mode
Decision question
Which measurable production or release decision must the evidence support for this case: Detect Adhesive Dispensing Defects Early?
Keep separate
Treat the relevant evidence streams separately before correlating them: Width, height, position, and volume; Use dispensing data; Add inspection for hidden defects.
Credible reference
A missing segment, volume error, and poor wetting do not always arise at the same point. We separate bead geometry, mix ratio, and joint effect. Use marked known-good and known-failed parts, the applicable functional limit, and recorded process data as the shared reference set.
Next step
Begin with a small, correlated feasibility set. Prove that width, height, position, and volume relates to the required function before defining a series method, threshold, or cycle time.
Choose the right inspection strategy
Non-destructive inspection or targeted destructive testing?
Non-destructive testing (NDT) examines a component without inherently making it unusable. Destructive methods such as sectioning, tensile, peel, burst, or fracture tests consume or permanently alter at least one specimen. Both have a valid role; the strongest commercial route is often a deliberate combination.
Non-destructive testing
- Evidence on the real component, often without extensive specimen preparation
- Measurements can be repeated and compared over the process history
- Suitable for rapid screening, sorting, and—after validation—series inspection
Destructive testing
- Provides direct mechanical, material, or microscopic reference evidence
- Important for root-cause work, thresholds, and validating an NDT signal
- Often needs specimen preparation, conditioning, and replacement parts
Parts often do not need to be cut, prepared, or replaced after the test. Measurements can be repeated, automated, and moved closer to the line, reducing sample logistics, waiting time, and feedback delay.
Lower inspection scrap, less preparation, and higher throughput reduce cost per evaluated part. With expensive components or high volumes, the saving occurs across the process—not only in the laboratory.
For a credible proposal
What specialists need
A specialist can usually prepare a credible first proposal from adhesive system, bead geometry and tolerance, surface, robot path, takt time, variants, known defects, access, and traceability needs. Photographs, a marked drawing, a short process map, and a small table of good and bad cases are often more useful than a long narrative without traceability.
The request should state the deliverable. Examples include a feasibility result, an inspection report, a root-cause hypothesis, a confirmed cause, a validation plan, a production concept, or a priced implementation. Sample quantity, location, deadline, confidentiality, shipment constraints, and the person who can answer technical questions complete the commercial scope.
Unknown information may remain unknown. eXalt® records open points explicitly and turns them into clarification questions instead of silently inserting assumptions. That is important for comparable quotes because each supplier can see the same evidence, exclusions, and expected outcome.
Transparent, not falsely precise
What drives cost and turnaround
Cost and lead time are driven by the number and condition of samples, preparation, fixtures, access, method combination, reference defects, production access, travel, repeat runs, engineering interpretation, and report depth. The technical path described here—2D and 3D vision, laser profiling, flow and pressure monitoring, weight checks, thermal imaging, and destructive references—may be offered in stages when feasibility is not yet proven.
Comparable quotes should separate intake and test planning, the initial measurement or trial, optional escalation, reporting, and any production-transfer work. Fixtures, sample manufacture, travel, data export, repeat measurements, and destructive confirmation should be named rather than hidden in one total. A limited feasibility study is more honest than a full-system quote built on an untested assumption.
Schedule risk often sits outside instrument time. Sample shipment, security approval, fixture design, reference-part creation, access to a production window, and internal decision cycles can dominate elapsed time. eXalt® does not display invented market prices or fabricated lead times. Only actual quotes and recorded outcomes are treated as marketplace data.
My decision guide
How to select the right path and compare quotes
I would compare suppliers on four evidenced requirements. The supplier must show that it understands the observed failure, can demonstrate the required detection or measurement capability, offers a plan that leads to the buyer's decision, and states scope, limitations, outputs, and next steps explicitly. If one of those requirements is missing, the proposal is not yet defensibly comparable. A low-priced test is not economical if it leaves the cause open or forces a second supplier to repeat the work.
Do you need to know the exact technology before submitting a request? No. A real problem, its boundary conditions, and the decision you need are enough to start. Is a photograph alone sufficient? Usually not, but it can make the first triage much faster when it is paired with part context and a good-versus-bad definition.
The practical sequence is simple: describe what actually happens, preserve the evidence, define the decision, and let qualified specialists propose the proof path. CorDev then places the proposals into a common structure so method, assumptions, timing, exclusions, and price can be compared without turning the journey into a horizontal vendor directory.
Answered briefly
Common questions about technical manufacturing problems
Does the cause need to be known?
No. Describe the expected-versus-actual result, process step, frequency, conditions and required decision.
Which documents help at the start?
Photographs, drawings, good and failed parts, process data, prior attempts and known changes shorten the investigation.
How does a problem become a defensible next step?
Prioritize hypotheses, connect each to suitable evidence and define clear decision or stop criteria.
Does submission create a paid order?
No. The request first supports qualification and supplier discovery. A paid order only exists after a later, explicit agreement.